Presence
Confirm that the required component, product or pack item is present.
 Discuss a requirement
Vision inspection within Integration
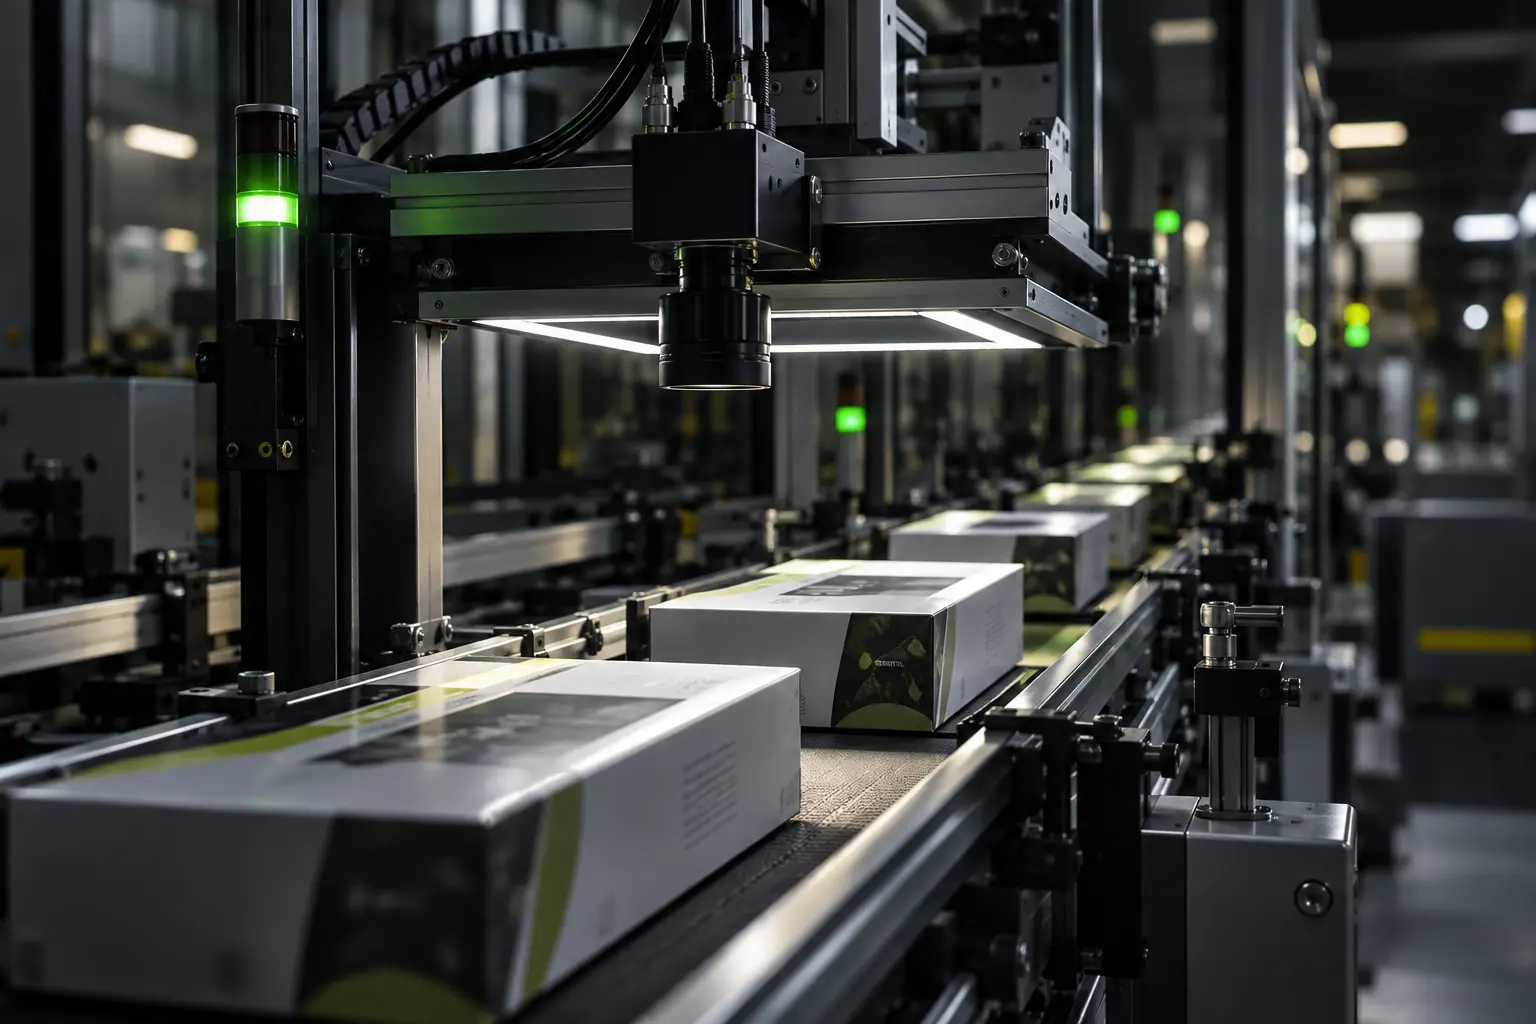
Machine vision checks the details that identity alone cannot confirm. It can inspect presence, count, position, labels, packaging and product condition.
What the camera must decide
The right vision system combines lighting, optics, processing and rejection logic around a clearly defined inspection event.
Confirm that the required component, product or pack item is present.
Check that the expected quantity is complete before the process moves forward.
Verify placement, orientation and alignment against the production rule.
Validate the right label, code or printed element where it must appear.
Check closure, completeness and visible packaging condition.
Identify visible defects and classification differences at operational speed.
Vision plus identity
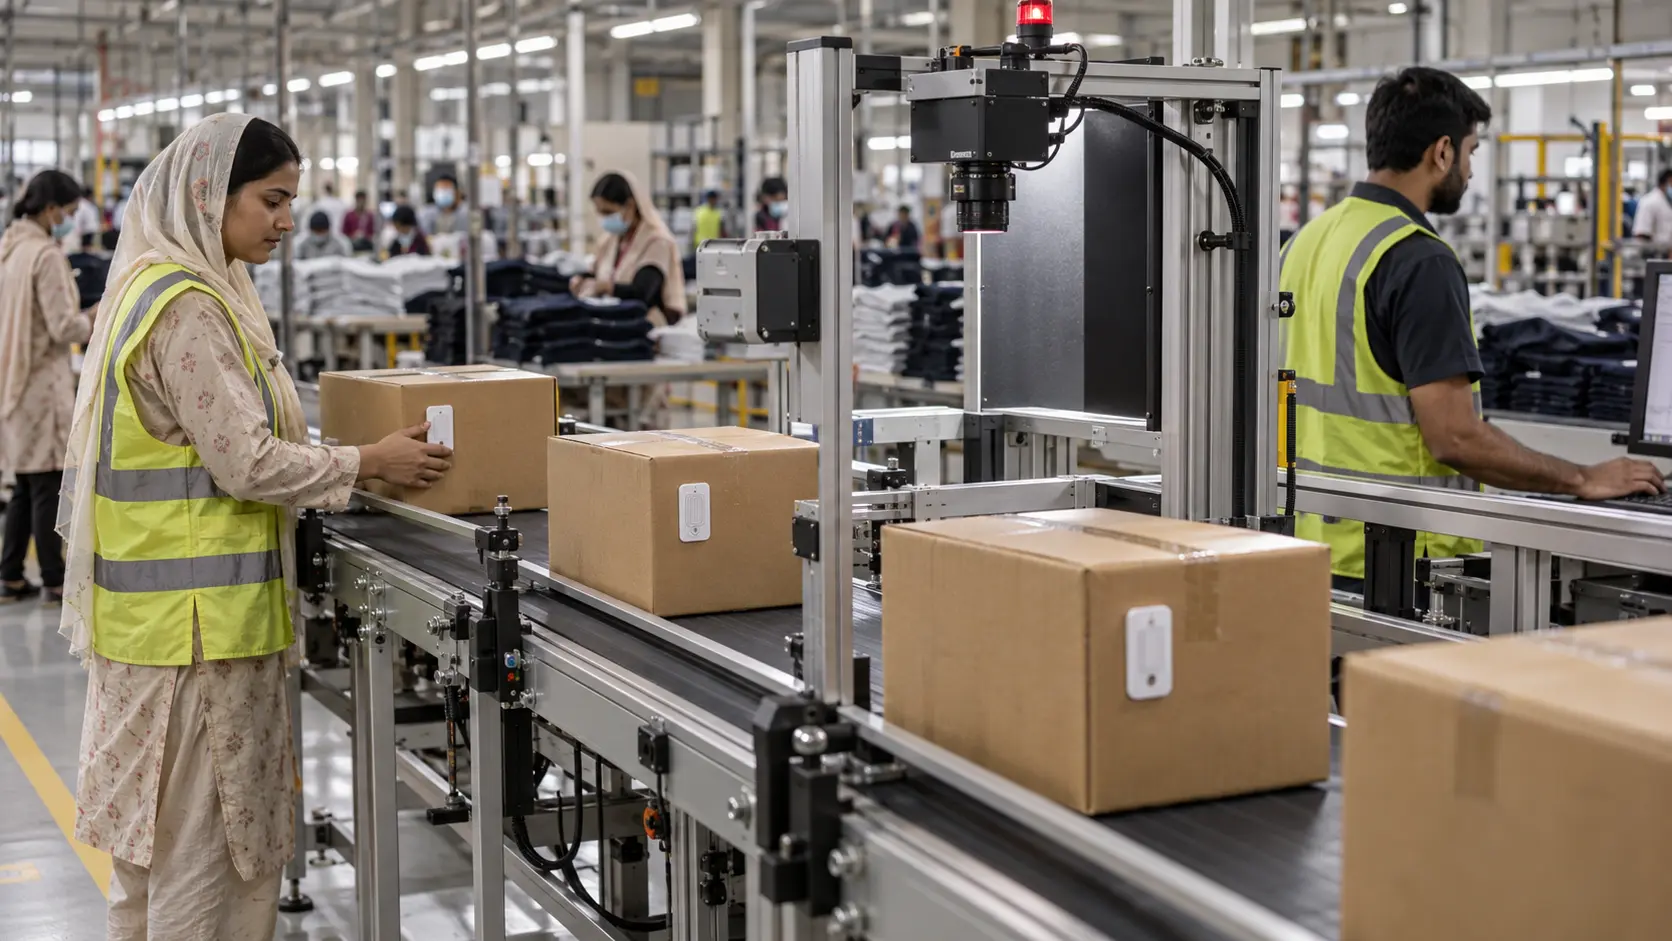
When vision and traceability work together, an inspection result can become part of the product record. This supports stronger evidence and faster exception handling.
Inspection architecture
Consistent inspection depends on the full environment rather than the camera alone.
Translate the operational concern into a visual rule that can be tested.
Choose lighting, lens, position and trigger conditions around the product.
Use the right vision method to classify the result and identify exceptions.
Record, reject, alert or stop the process according to the required response.
Inspection becomes more useful when the result belongs to the product history.
Share the product, the defect and the speed of the process.